

Ensuring the legibility of Data Matrix codes is not merely a matter of getting a handheld scanner or a station camera to capture the code’s content at a given moment. For plant managers, the priority lies in verifying that the marking complies with industry-standard metrics and will withstand the most demanding operational conditions.
Industrial traceability requires that every part manufactured from metal or engineering plastics can be identified without error throughout its entire service life. On modern production lines, direct marking on the surface ensures the permanence of the information but poses extraordinary reading challenges due to the variety of reflections, textures, and finishes—which is why a process for verifying Data Matrix codes is carried out.
That said, as specialists in industrial marking and traceability solutions, at COUTH we have developed this technical guide aimed at process engineers, quality managers, and production directors. In it, we cover the methodology for evaluating, interpreting, and validating the quality of direct marking in highly demanding environments.
Reading, Verifying, and Validating Markings
Operational Differences Between Reading and Verification
In the manufacturing sector, there is common confusion between the act of reading a code and the discipline of verifying it. Reading involves checking whether a specific scanner or optical reader is capable of decoding the information under specific conditions of lighting, distance, and angle. This test only demonstrates that that particular device captured the data at a specific moment.
However, the fact that a shop-floor reader captures the information does not guarantee that the part can be identified by other automated systems later on. If the angle of the light, surface wear, or the technology of the destination scanner changes, a defective mark will cause unplanned stoppages on the assembly line.
In contrast, Data Matrix code verification is a metric and standardized procedure that uses properly calibrated inspection devices. By applying international standards, this analysis measures the physical quality of the mark and assigns an objective rating that is independent of the reader used.
Process Validation as a Guarantee of Repeatability
While Data Matrix code verification evaluates an individual part at a single point in the workflow, validation ensures the stability of the marking system over time. Validation involves establishing a preventive protocol that certifies that micro-percussion, engraving, or laser technology consistently produces compliant codes during every shift.
To achieve a validated process, quality departments must define periodic sampling guidelines and monitor the progression of wear on marking tools. This prevents gradual deviations that could ultimately affect entire production batches.
An effective validation program allows for the detection of variations in raw material hardness or minor misalignments in tooling before they affect production. At COUTH, we design our equipment with this in mind, which is why we integrate control loops that facilitate this continuous monitoring without slowing down the factory’s pace.
How to Verify a Code Marked Directly on the Part (DPM)
Metrological requirements for metal parts and engineering plastics
Direct part marking (DPM) presents specific challenges not found in conventional labeling on paper or cardboard. The low reflectance of steels, the gloss of aluminum alloys, or the rough textures of castings alter the way light is projected onto the matrix.
For this reason, not just any commercial inspection system can be used to verify a Data Matrix code marked on a rough or polished part. A verifier equipped with specific lighting configurations (such as diffuse light, domes, or light sources at 30, 45, or 90 degrees) capable of revealing the actual relief of the marking is required.
These advanced optical configurations allow the marking features to be isolated from the imperfections inherent in the base material. This ensures a clean analysis of the marked modules, guaranteeing repeatable measurements that align with real-world operating conditions.
Inspection Protocol Based on International Standards
The metrological evaluation for verifying Data Matrix codes on industrial parts is governed by the ISO/IEC TR 29158 (AIM DPM) standard, specifically designed to address the complexity of readings on hard surfaces. This standard adapts the criteria of the ISO/IEC 15415 standard to the specific characteristics of surface relief and direct contrast.
During the analysis process, the calibrated equipment captures an image of the symbol and evaluates multiple metrics using standardized algorithms. Key factors examined include cell contrast, modulation, minimum reflectance, and geometric distortion of the axes.
Conducting the inspection using this approved methodology allows for the certification of each batch’s quality through auditable reports. This documentation is essential for meeting the requirements of global customers in highly regulated industries.
Interpretation of Data Matrix Code Quality Grades
The ISO/IEC TR 29158 Rating Scale
The result obtained after the metrological inspection is expressed as a Data Matrix quality grade represented by a letter (A, B, C, D, F) or an equivalent numerical value on a descending scale from 4.0 to 0.0. Each analyzed parameter receives its own score, with the lowest grade determining the symbol’s overall score.
- A grade A (4.0) indicates a perfect mark, with optimal contrast and flawless geometry, while a grade B (3.0) or C (2.0) certifies a compliant code, but with minor, tolerable variations. Below these levels, reading reliability decreases dramatically.
- A code rated D (1.0) is considered marginal and presents a high risk of failure if the part is exposed to dirt or lubricants. Meanwhile, a grade F (0.0) represents a rejected marking that does not meet the minimum thresholds required by the industry.
Acceptance Criteria Based on Environment and Application
Understanding quality grades allows process engineers to set acceptance thresholds tailored to the product’s actual lifecycle. Not all parts require an A grade; however, it is essential to establish limits that prevent the release of defective components.
For example, for parts exposed to subsequent machining, painting, or heat treatment processes, it is advisable to require starting grades of A or B. This ensures a sufficient safety margin against the inevitable degradation the surface will undergo.
Clearly defining acceptance criteria in the inspection guidelines prevents unjustified rejections of perfectly functional parts. At the same time, it prevents the use of codes with low legibility that would ultimately fail at final assembly plants.
Physical parameters evaluated during testing
1. Cell contrast and modulation
Cell contrast measures the difference in reflectance between the light and dark modules that make up the matrix. In micro-percussion or laser marking on metal, this contrast is not achieved through color changes, but rather through the scattering of light caused by surface deformation or micro-melting.
On the other hand, modulation examines the uniformity of reflectance throughout the entire code. If there are variations in the depth of the notches or areas where the relief is less pronounced, the modulation decreases, leading to errors in the Data Matrix code as the scanner misinterprets the code modules.
Ensuring high Cell Contrast (CC) and Modulation (MOD) through the precise adjustment of COUTH’s marking parameters guarantees immediate readability under any workshop lighting conditions.
2. Geometry, Finder Pattern, and Quiet Zone
The code geometry encompasses the straightness of the axes, the roundness of the printed dots, and the alignment of the grid. Axial or grid distortion is typically caused by vibration of the part during marking or by improper tool positioning.
The Finder Pattern, consisting of two continuous “L”-shaped lines, is critical for the reading software to locate and identify the code’s orientation. If this structure is damaged or distorted, automatic decoding will be impossible.
Finally, the Quiet Zone is the mark-free margin that must completely surround the code. Maintaining this clear perimeter is essential to prevent the part’s textures, chamfers, or edges from interfering with the capture of the matrix.
What causes an illegible mark on the production line?
Mechanical factors and wear on marking equipment
A progressive degradation of the stamp impression is often a sign of mechanical misalignment in marking systems.
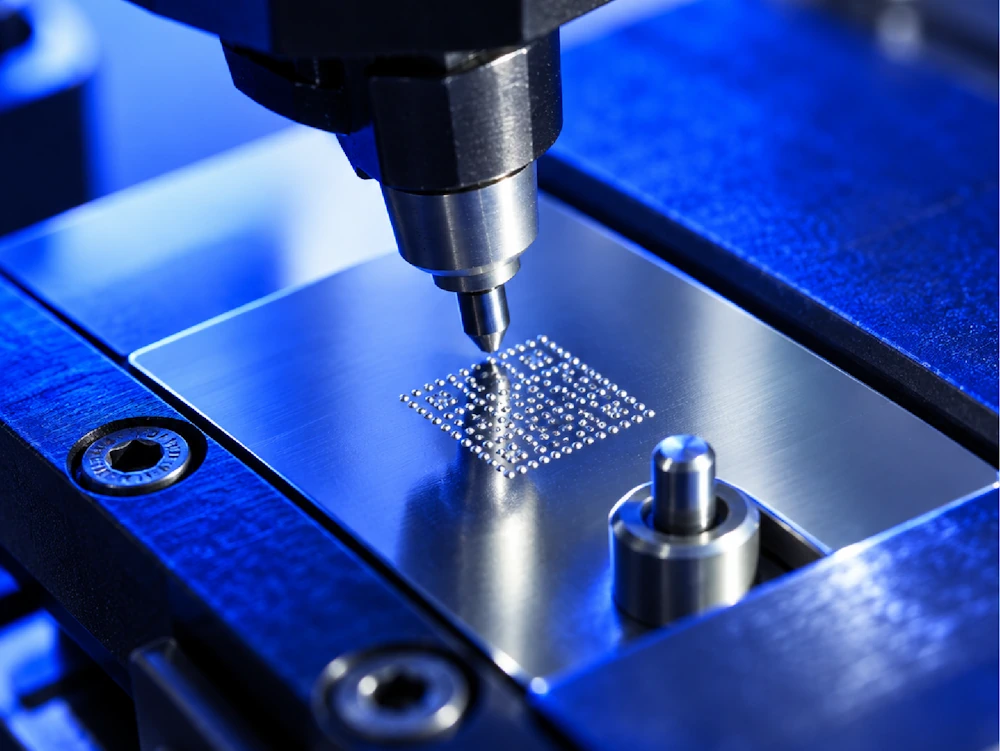
- In micro-percussion technology, wear on the carbide tip or deterioration of the impact spring reduces the depth of the dot, altering the code’s geometry and consequently the readability of the Data Matrix.
- In the case of laser marking, soiling of the protective lenses or a loss of focus at the focal length reduces the energy density delivered to the part. This loss of power affects thermal contrast and creates blurred edges in the matrix modules.
Likewise, a lack of rigidity in the clamping fixtures causes microvibrations during the marking cycle. This unintended movement of the part causes grid distortions that prevent reading by automatic inspection systems.
Influence of Metallurgy and Surface Finishes
Variability in the properties of the raw material directly affects the performance of the marking technology. Unanticipated changes in steel hardness, casting grain size, or material roughness alter the surface’s reaction to impact or the light beam, causing errors in Data Matrix codes.
Similarly, the presence of machining oils, coolants, protective greases, or talc residue on plastic parts alters the substrate’s reflectance. These intermediate layers scatter the reader’s light and cause unintended capture errors.
Anticipating these process variations through the proper selection of power, frequency, and impact geometry ensures stable and durable marking that withstands normal material fluctuations on the production floor.
Impact of Post-Marking Treatments on Readability
Coatings, Paint, and Electroplating
In the manufacturing industry, it is common for parts to undergo finishing treatments after the marking process. Operations such as anodizing, cataphoresis (KTL), zinc plating, electroplating, or powder coating deposit layers that significantly alter the topography of the mark.
- If the initial relief depth is insufficient, the coating fills in the cavities of the mark and smooths out the edges of the modules. As a result, the optical contrast disappears completely beneath the paint layer, making it impossible to decode the content.
- When verifying Data Matrix codes beneath these protective coatings, a shallow mark will cause critical reading errors at automatic inspection stations.
To prevent this loss of traceability, COUTH designs marking strategies with depths and dot profiles adapted to the thickness of the overlying layer. This ensures that the code retains the necessary relief and contrast to be read after treatment.
Heat-Treatment Hardening Processes
Carburizing, quenching, tempering, or shot blasting processes subject metal components to extreme thermal and mechanical stresses. These operations cause surface oxidation, darkening of the metal, and minor dimensional changes in the part.
Sandblasting or cleaning shot blasting subsequently erodes the surface and may round off the edges of the marked modules. If the matrix has not been generated with the appropriate parameters, this abrasive process will cause errors in the Data Matrix by destroying the symbol’s geometric structure.
Considering the component’s entire life cycle before defining the marking recipe is the only way to ensure permanent identification of parts from forging or machining through to final replacement.
What are the operational consequences of poor marking?
1. Direct costs, rejects, and line stoppages
Allowing components with marking defects to move through the production line generates extraordinary costs that directly impact the manufacturing margin. A failed read at an automatic station halts the flow of the robotic cell and requires manual intervention by the operator.
This interruption reduces the plant’s OEE (Overall Equipment Effectiveness) and causes unforeseen issues that seriously affect the readability of Data Matrix codes at subsequent inspection points, also forcing manual data re-entry with the consequent risk of human error.
In the worst-case scenario, if the defective marking is not detected in time, the part will be processed in its entirety only to be rejected during final inspection, wasting the added value from machining, assembly, and energy.
2. Penalties and Loss of Customer Certification
In highly integrated sectors such as the automotive or aerospace industries, shipping components without the appropriate level of Data Matrix quality constitutes a serious breach of the end customer’s specifications. These incidents often result in the return of entire containers and logistics penalty charges.
In addition to direct financial losses, the accumulation of traceability incidents affects the supplier’s quality rating. A negative evaluation in this area jeopardizes participation in new projects and may even lead to the loss of commercial certification due to repeated Data Matrix errors.
Therefore, investing in control and verification systems at the source transforms traceability into a competitive advantage, projecting an image of maximum reliability and rigor to the global market.
COUTH Methodology for Quality Control on Production Lines
To prevent the spread of identification errors, the best strategy is to perform a rigorous verification of Data Matrix codes immediately after they are printed. COUTH’s solutions allow for the integration of intelligent vision cameras and calibrated verifiers directly into the print head or the workstation itself.
This inline configuration inspects 100% of production without adding cycle time to the operation. By capturing the image in milliseconds, the software analyzes the matrix and determines the readability of the Data Matrix to validate the symbol’s compliance before the part leaves the clamping fixture.
If the system detects a trend toward degradation or a code outside tolerance, the line can automatically stop or divert the component to a reject bin, preventing the defect from affecting the rest of the batch.
Preventive Maintenance and Calibration Plans
Any metrology inspection equipment requires a structured maintenance and calibration program to ensure that its readings remain objective and reliable over time. Deviations in lighting or lens contamination alter measurements and directly affect the accuracy with which the Data Matrix quality grade is assessed, potentially leading to false rejections.
Quality managers must schedule periodic cleanings of the optical components and perform calibration tests using approved standards or test charts. This procedure confirms the stability of the vision sensor and validates the repeatability of the measurement.
By following the maintenance guidelines provided by COUTH, industrial plants ensure the operational continuity of their marking and vision equipment, maximizing line availability and guaranteeing audit-proof traceability.
